Haze, Slow Filtration and Thick Mash: A Troubleshooting Guide for Fruit Processors
For fruit processors fighting persistent haze, filters that block early and high viscosity. What to check first, how to run dose trials, and what to send for a bulk quote.
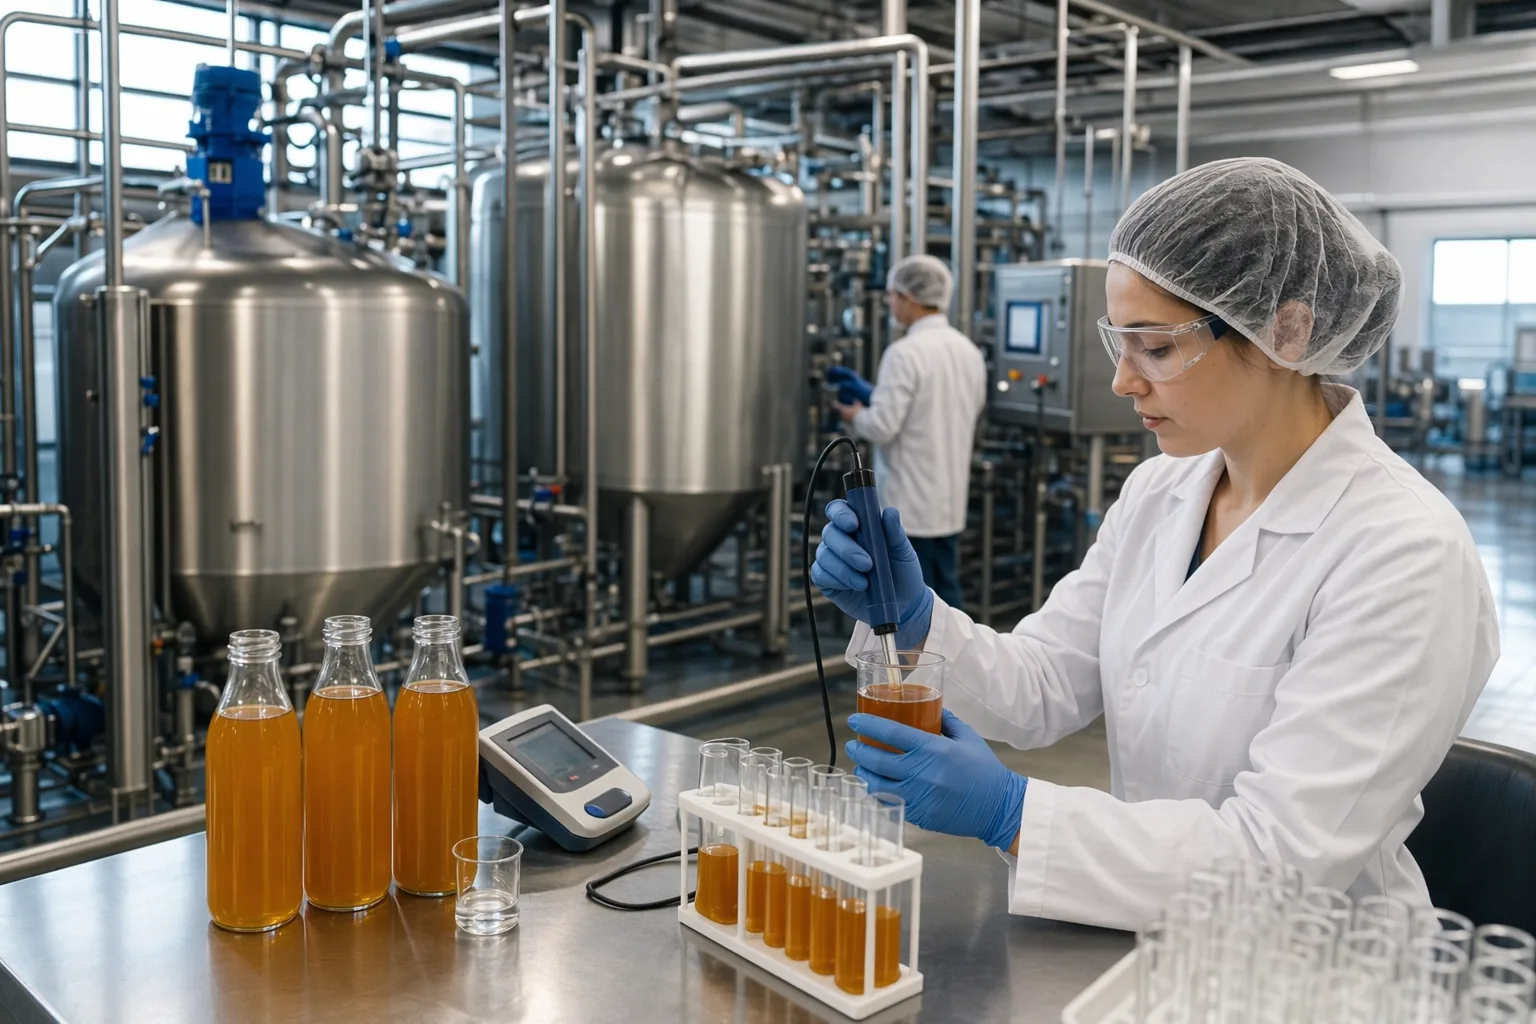
For production, QA and purchasing teams at juice, concentrate and fruit processing plants: haze that will not clear, filters that block early and mash that stays thick all cost line time and filter aid. This guide shows what to check first, how to run a dose trial, and how to pick a supplier that supports the trial.
To request a quote, send the product (liquid or powder), the quantity, the destination and your process step to hello@mail.freshenzyme.com or through the inquiry form. Packs are 25 kg drums, 200 L barrels or custom packaging; the minimum order is 25 kg; pricing and freight are quoted per order.
Why Juice Clarification Fails in Production
Cloudy juice, slow filtration, poor yield, and unstable haze are often caused by residual pectin, suspended pulp, starch interactions, or insufficient enzyme contact. In apple, berry, tropical fruit, and grape processing, pectin forms a colloidal network that increases viscosity and traps fine solids. A juice clarification enzyme based on pectinase breaks down pectic substances so particles settle or filter more efficiently. When clarification fails, the issue is not always enzyme quality; it may be incorrect pH, low temperature, short holding time, weak mixing, enzyme addition after heat damage, or fruit maturity variation. A clarification enzyme should therefore be treated as a process control tool, not a simple additive. Troubleshooting begins with mapping the fruit type, Brix, pH, pulp load, thermal history, tank geometry, and downstream separation method.
Common symptoms: haze, high viscosity, low press yield, slow filter flow, unstable concentrate. • Root causes often include pectin load, poor mixing, wrong temperature, or insufficient reaction time. • Fruit maturity and storage conditions can change enzyme demand from batch to batch.
Starting Conditions for Plant Trials
Safe starting conditions should come from the product TDS, then be confirmed in a plant or pilot trial. Our juice clarification enzyme is specified for pH 3.5–5.5 and 40–55 °C; holding time is set in the trial. Lower temperatures may work but usually require longer contact time or higher dosage. Excessive heat can reduce enzyme activity, especially if the enzyme is added before hot-fill, pasteurization, or evaporation steps. Dosage bands vary by activity unit and formulation, so processors begin with the supplier-recommended range per metric ton of mash or juice, then optimize based on data. The best dosage is rarely the highest dosage; it is the level that achieves target clarity, throughput, and yield at the lowest cost-in-use.
Confirm dosage by enzyme activity, not only by product weight or volume. • Add enzyme with good agitation to avoid localized under-treatment. • Run side-by-side controls against untreated juice and current plant practice.
Dosage Strategy for Plant Trials
Screen around the supplier’s recommended range, which is based on enzyme activity units and juice composition. High-pectin fruits, concentrated mash, low-temperature processing, or short residence time may require the upper end of a trial range. Lower-pectin juices or longer holding times may need less. Because commercial products differ in activity, do not compare dosage only by weight; compare performance, cost-in-use, and declared activity where available. A good pilot validation uses untreated control, low dose, target dose, and high dose samples under the same pH, temperature, and contact time. Track clarity and filterability over time rather than relying on a single visual check. This prevents under-dosing, over-dosing, and unnecessary enzyme spend.
Start with supplier TDS dosage, then bracket lower and higher trial points. • Use identical mixing, time, temperature, and sample volume for each trial. • Calculate enzyme cost per metric ton or per 1,000 liters of juice.
QC Checks That Show Whether the Enzyme Is Working
Reliable troubleshooting requires measurable checkpoints before and after treatment. In apple juice clarification, for example, an alcohol pectin test can indicate residual pectin, while viscosity and NTU turbidity show whether the juice is becoming easier to clarify. Filterability tests, centrifuge spin tests, sediment volume, press yield, and flow rate through membrane or plate filters provide process-level evidence. For wine and grape juice, monitor clarification without stripping desired mouthfeel or aroma. For fruit processing concentrates, check whether enzyme treatment improves evaporation stability and reduces fouling. Document Brix, pH, temperature, dose, time, and agitation for every trial. If turbidity decreases but filtration remains slow, the issue may involve starch, protein-polyphenol haze, fine pulp, or inadequate fining rather than pectin alone.
Track NTU, viscosity, filterability, sedimentation, yield, and sensory impact. • Use a blank control and a current-process control in every trial. • Retain samples through shelf-life or concentrate storage when stability matters.
Troubleshooting Dosage, pH, and Temperature Problems
If wine must, apple juice or another fruit stream does not clarify as expected, adjust one variable at a time. A low response may indicate pH outside the enzyme window, temperature below the recommended range, heat-inactivated enzyme, inadequate mixing, or fruit with unusually high pectin. If clarification improves but flavor or color changes undesirably, reduce holding time, lower dosage, or review oxidation control and fining steps. When filtration is still slow after pectin breakdown, test for starch, protein, gums, or excessive fine solids. The enzyme should also be checked for compatibility with preservatives, fining agents, bentonite, activated carbon, and process aids. Always validate at pilot scale before full production changes, then lock the operating range into batch records, QC release criteria, and operator instructions.
Change dose, pH, temperature, or time individually to identify the true driver. • Do not add enzyme immediately before a high-heat step unless the process is validated. • Use plant data to define minimum effective dosage and maximum practical holding time.
Selecting a Supplier for Juice, Wine, and Fruit Processing
A qualified supplier should support both technical performance and procurement risk control. Ask for the COA for each lot, a TDS with activity definition and recommended operating window, and an SDS for handling and storage. For wineries, evaluate whether the supplier can provide guidance for grape variety, must temperature, pressing style, and clarification target. For puree, concentrate, and mash operations, the supplier should understand pulp load, press extraction, decanter behavior, and evaporator performance. Avoid supplier selection based only on unit price. Compare cost-in-use by calculating enzyme dose, treatment time, yield gain, filter aid reduction, energy savings, and line throughput. Pilot validation is essential because different fruits and seasons can require different enzyme profiles.
Request COA, TDS, SDS, storage conditions, shelf-life, and lot traceability. • Confirm technical support for pilot testing and scale-up. • Evaluate cost-in-use, not only price per kilogram or liter.
What to Send With a Quote Request
A quote request that contains the following gets a usable answer in one reply instead of several rounds of questions. Distributors and resellers can send the same details for their end customer's application.
Product form: liquid or powder, and the activity range you work with. • Quantity: first order and expected monthly or annual volume. • Destination: country and port or delivery city, so freight can be quoted. • Process: fruit or must, treatment point (mash, juice or must), temperature, pH and holding time. • Documents your QA team needs to review before approval. • Pack preference: 25 kg drums, 200 L barrels or custom.
Buyer Questions
There is no universal dosage because enzyme activity, fruit variety, pectin load, pulp level, pH, and temperature all affect performance. Start with the supplier TDS recommendation, then run bench or pilot trials across a dosage band. Measure NTU, viscosity, filterability, yield, and sensory impact. The approved dose should be the lowest level that consistently meets clarification and throughput targets.
Persistent haze can result from under-dosing, short contact time, poor mixing, low temperature, pH outside the enzyme range, or enzyme deactivation by heat. It can also come from non-pectin haze such as starch, protein-polyphenol complexes, gums, or fine pulp. Run an alcohol pectin test, turbidity test, viscosity check, and filterability comparison before changing the process.
Sometimes, but validation is required. Apple juice clarification, grape must treatment, wine clarification, berry juice, and tropical fruit processing can have different pectin structures, phenolic profiles, temperatures, and sensory requirements. A pectinase juice supplier for wine or fruit processing should provide application guidance, but your plant should confirm dosage, time, and quality results with pilot testing.
Request the COA for the supplied lot, TDS with activity definition and operating conditions, SDS for handling and storage, shelf-life information, recommended storage temperature, and lot traceability details. For supplier qualification, also ask for technical support on pilot validation, change notification practices, and practical guidance on cost-in-use analysis for your fruit and process line.
Cost-in-use includes more than enzyme price. Calculate the enzyme cost per metric ton of juice or mash, then include yield improvement, reduced filter aid, shorter clarification time, increased filtration flow, lower rework, and potential energy savings. Compare treated and untreated trials using the same fruit lot when possible. The best option is the enzyme program that delivers stable quality at the lowest total process cost.
Juice Clarification Enzymes for Research & Industry
Need Juice Clarification Enzymes for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
What dosage should we use for pectinase juice for juice clarification?
There is no universal dosage because enzyme activity, fruit variety, pectin load, pulp level, pH, and temperature all affect performance. Start with the supplier TDS recommendation, then run bench or pilot trials across a dosage band. Measure NTU, viscosity, filterability, yield, and sensory impact. The approved dose should be the lowest level that consistently meets clarification and throughput targets.
Why is our juice still cloudy after adding pectinase?
Persistent haze can result from under-dosing, short contact time, poor mixing, low temperature, pH outside the enzyme range, or enzyme deactivation by heat. It can also come from non-pectin haze such as starch, protein-polyphenol complexes, gums, or fine pulp. Run an alcohol pectin test, turbidity test, viscosity check, and filterability comparison before changing the process.
Can the same pectinase be used for apple juice, wine, and fruit processing?
Sometimes, but validation is required. Apple juice clarification, grape must treatment, wine clarification, berry juice, and tropical fruit processing can have different pectin structures, phenolic profiles, temperatures, and sensory requirements. A pectinase juice supplier for wine or fruit processing should provide application guidance, but your plant should confirm dosage, time, and quality results with pilot testing.
What documents should we request from a juice clarification enzyme supplier?
Request the COA for the supplied lot, TDS with activity definition and operating conditions, SDS for handling and storage, shelf-life information, recommended storage temperature, and lot traceability details. For supplier qualification, also ask for technical support on pilot validation, change notification practices, and practical guidance on cost-in-use analysis for your fruit and process line.
How do we calculate cost-in-use for industrial pectinase juice?
Cost-in-use includes more than enzyme price. Calculate the enzyme cost per metric ton of juice or mash, then include yield improvement, reduced filter aid, shorter clarification time, increased filtration flow, lower rework, and potential energy savings. Compare treated and untreated trials using the same fruit lot when possible. The best option is the enzyme program that delivers stable quality at the lowest total process cost.
Related: Clearer Fruit Juices with Faster Separation
Turn This Guide Into a Supplier Brief Contact Fresh Enzyme to discuss COA/TDS/SDS review, pilot validation, and cost-in-use optimization for your juice clarification process. See our application page for Clearer Fruit Juices with Faster Separation at /applications/fruit-juice-clarification/ for specs, MOQ, and a free 50 g sample.
Contact Us to Contributehello@mail.freshenzyme.com